Expansion projects rarely fail because the new machine was misunderstood. More often, the problem sits around it: a compressed-air header that loses pressure during shift overlap, a chilled-water loop designed for yesterday’s heat load, a warehouse aisle that turns every material changeover into a queue, or a transformer with no credible margin for the next process upgrade.
Manufacturing infrastructure analysis gives project managers and engineering leads a disciplined way to expose these constraints before they become commissioning delays, unstable quality, missed output targets, or unplanned capital requests. It connects the production line to the less visible systems that make production possible—power, steam, water, ventilation, drainage, compressed air, material movement, digital controls, and maintenance access.
For specialized manufacturing environments such as textiles, printing, papermaking, food-contact packaging, and converting, the exercise is especially important. These operations often combine continuous processes, variable product mixes, high utility demand, sensitive quality parameters, and equipment supplied by multiple vendors. A line may look balanced on a layout drawing while remaining fundamentally unbalanced in real operating conditions.
Start with the operating promise, not the equipment list
A useful analysis begins with a question that is more demanding than “Can the plant fit the equipment?”: What operating result must this facility reliably deliver? The answer should describe product families, target throughput, shift pattern, expected uptime, quality requirements, changeover frequency, and future expansion horizon.
This matters because nameplate capacity is not the same as usable capacity. A printing line rated for a certain speed may be constrained by ink preparation, drying energy, roll handling, color approval, or downstream inspection. A packaging line can appear to have surplus machine time while its output is limited by carton supply, palletizing capacity, warehouse staging, or food-safety sanitation windows. In papermaking and tissue conversion, stock preparation, steam balance, water treatment, and reel logistics may govern the practical ceiling more than the finishing machine itself.
Translate the operating promise into a small set of design-basis statements. For example:
- Required saleable output per hour, shift, and year—not simply gross machine output.
- Product-mix assumptions, including the share of short runs, customized orders, and high-specification products.
- Planned availability after routine maintenance, cleaning, grade changes, and quality holds.
- Utility conditions needed at the point of use: voltage, pressure, temperature, purity, flow, and continuity.
- Recovery expectations after a trip, utility interruption, or upstream material shortage.
These statements give every later calculation a common reference point. Without them, teams may compare individual equipment capacities that were never intended to operate under the same conditions.
Find the real bottleneck: flow, variability, and loss accumulation
The narrowest point in a process is not always the bottleneck. A machine with the lowest nominal throughput may be predictable and well protected by buffer capacity. Conversely, a fast asset with frequent stops, difficult restart conditions, or variable utility demand can set the pace for the whole operation.
Map the process from receiving through dispatch, including intermediate storage, inspection, rework loops, and waste handling. For each stage, record four practical measures: effective rate, uptime, changeover or cleaning time, and buffer availability. Effective rate should account for scrap, quality downgrades, planned stoppages, and normal operating speed—not the number on a vendor brochure.
A simple capacity relationship is:
Effective capacity = nominal rate × operating availability × yield × scheduled operating time.
The formula is not a substitute for a simulation model, but it quickly reveals misleading assumptions. If a converting line has ample mechanical speed but loses substantial time to roll changes, adhesive preparation, inspection rejects, and downstream pallet congestion, increasing the line’s rated speed may add little saleable output.
Look carefully at queues. A persistent queue before one process, paired with starvation after it, is strong evidence of a constraint. Yet queues must be interpreted in context. Intentional buffers can protect a continuous upstream process from a batch-oriented downstream station. The concern is uncontrolled accumulation: work-in-progress that consumes floor space, obscures quality status, raises damage risk, and makes production performance harder to see.
Why peak demand deserves more attention than annual averages
Annual consumption figures are useful for budgeting, but commissioning failures occur at peaks. A textile finishing operation may experience simultaneous demand when dryers, pumps, extraction systems, and compressed-air users ramp together. Digital printing may create coincident electrical loads through curing, HVAC, and data-intensive inspection. In food packaging, washdown and sanitation can shift water and drainage demand into periods that were not represented in average production calculations.
For each major system, analyze at least three conditions: normal production, credible peak production, and abnormal-but-plausible recovery conditions. The third condition is often missed. When several machines restart after a short outage, inrush current, pressure decay, thermal load, and material demand can exceed what the system sees during steady operation.
Read utilities as process systems, not as site services
Utility infrastructure should be examined from source to point of use. A central plant can have sufficient installed capacity while the production asset still receives inadequate service because of undersized distribution lines, pressure losses, poor control logic, inadequate storage, or competing demand.
Measurement is usually more valuable than assumption. Temporary power loggers, ultrasonic air-flow measurements, pressure data loggers, thermal surveys, and production historian data can establish actual demand profiles. Where direct measurement is unavailable, engineering estimates should state their uncertainty and be tested during design review.
Quality conditions matter as much as quantity. Compressed air for pneumatic tools may tolerate conditions that are unacceptable for sensitive instrumentation or food-contact packaging. Water suitable for general cleaning may not be suitable for a process with strict color, hygiene, or deposit-control requirements. Treat utility specifications as process specifications.
Material handling is often the capacity calculation nobody completed
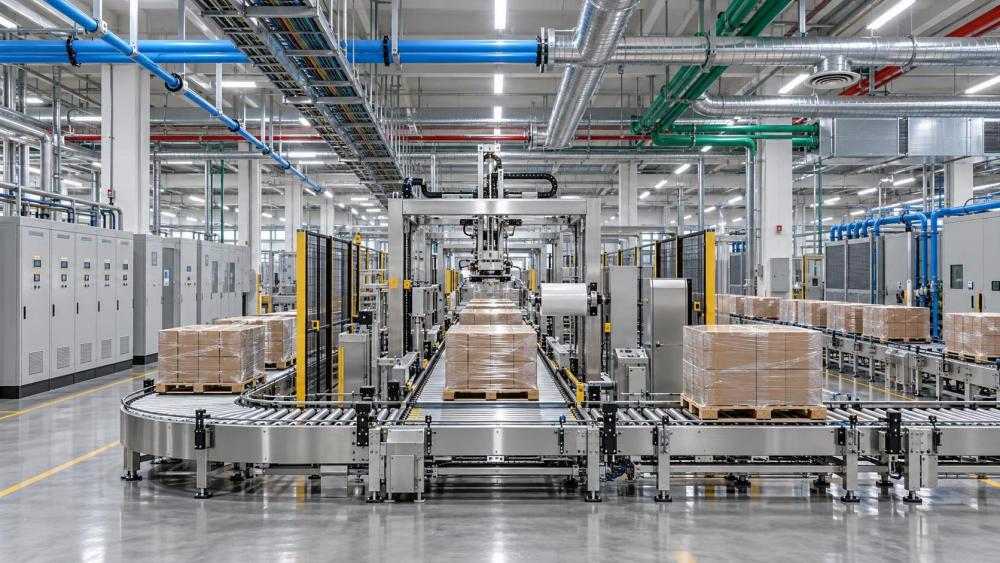
Project teams naturally focus on the main process equipment. But a line cannot sustain output if rolls, pulp, inks, boards, films, pallets, dies, chemicals, or finished goods cannot arrive and leave at the required rhythm. This is where physical layout becomes a production variable rather than an architectural drawing.
Review every movement: unloading, inspection, quarantine, storage, issue to line, return of unused material, waste removal, finished-goods staging, and dispatch. Consider travel distance, forklift interactions, aisle conflicts, lift capacity, loading dock cycles, and segregation requirements. For regulated or hygiene-sensitive packaging operations, also test the logic of people and material flows. A convenient shortcut may compromise clean-zone discipline or traceability.
Automated material handling deserves the same scrutiny as process equipment. Conveyor availability, accumulation logic, scanner reliability, pallet quality, and interface rules can govern the output of an otherwise capable line. In facilities moving toward customized production, the issue is often not raw transport speed but the ability to route many small, time-sensitive orders without losing identification or sequence control.
Use a bottleneck hierarchy to decide what to fix
Not every observed weakness deserves immediate capital spending. A mature manufacturing infrastructure analysis ranks constraints by their effect on safety, compliance, output, quality, energy, and recovery time. This prevents a common error: investing in the most visible problem rather than the one that limits overall performance.
One practical hierarchy separates issues into four categories:
- Hard constraints: conditions that physically prevent the target operating rate, such as inadequate electrical capacity, insufficient extraction, a too-small wastewater system, or a noncompliant fire-protection arrangement.
- Reliability constraints: assets that can meet demand in theory but have no redundancy, poor maintainability, obsolete controls, or single-point failures.
- Variability constraints: processes affected by product mix, inconsistent materials, long changeovers, unstable temperature or humidity, and manual coordination.
- Economic constraints: systems that work but consume disproportionate labor, energy, water, floor space, or working capital.
The order is not absolute. A reliability issue may deserve priority over a current throughput limitation if a failure would stop the plant for days. Likewise, a utility project may be justified by energy and emissions performance even where capacity is adequate. ISO 50001-style energy management principles can help teams establish baselines and identify significant energy uses, while local electrical, fire, environmental, and occupational safety requirements must remain the governing compliance reference.
Build scenarios instead of relying on a single “future state”
Long-term planning is uncertain, especially in sectors shaped by changing packaging regulations, fiber availability, digital print adoption, and demand for shorter runs. Rather than sizing all infrastructure against one optimistic forecast, create several operating scenarios: base demand, high-growth demand, high-mix demand, and constrained-utility demand.
Then ask what breaks first in each scenario. The answer may change. Under volume growth, the constraint may be steam generation or loading docks. Under high-mix production, it may be scheduling, cleaning capacity, ink kitchens, or material identification. Under a low-carbon transition scenario, electrical connection capacity and power-quality management may become more critical than legacy fuel infrastructure.
This approach supports staged investment. Some upgrades should be installed immediately because later modification would disrupt operations or require civil rework: buried utility corridors, structural provisions, drainage, cable routes, and reserved plant-room space. Other assets can be modular, such as additional compressors, pumps, treatment skids, or warehouse automation. The aim is not to overbuild; it is to preserve sensible options.
Turn findings into an execution-ready infrastructure plan
A good final report does more than identify “insufficient capacity.” It assigns each issue an owner, a confidence level, a required decision date, and a validation method. It should distinguish between measured facts, engineering assumptions, supplier claims, and open risks. That distinction is invaluable when schedules tighten and scope changes begin to compete for budget.
For every priority intervention, document the target condition, the dependency it removes, the tie-in requirements, expected shutdown window, commissioning test, and operating handover needs. Include controls integration and data visibility. In modern light industry, production and utility data should not remain in separate silos; energy spikes, pressure drops, humidity excursions, and line stops are often part of the same operational story.
GSI-Matrix approaches these questions through the lens of system integration: linking specialized process knowledge with the infrastructure and production equipment that determine real-world performance. For project leaders, that perspective is useful because it moves the conversation beyond isolated machines and toward an operating system that can support both mass output and increasingly customized production.
The most valuable outcome of manufacturing infrastructure analysis is not a larger list of capital projects. It is a clearer understanding of what the plant can reliably do, what conditions it depends on, and where a carefully chosen intervention will release capacity without creating a new constraint elsewhere. That clarity gives expansion projects a better chance to meet the promise made in the business case—on the first sustained production run, not months after handover.
Related News
- Industrial Trends Reshaping Equipment InvestmentMay 13, 2026Industrial trends are redefining equipment investment. Discover how automation, efficiency, modular design, and compliance shape smarter, lower-risk decisions.
- Greening Manufacturing: Where Energy Savings Pay BackMay 09, 2026Greening manufacturing starts with faster payback. Learn how integrated upgrades cut energy waste, improve uptime, and turn hidden efficiency gains into measurable factory returns.
- Manufacturing Infrastructure Analysis: Identifying Capacity and Utility BottlenecksSep 22, 2026Manufacturing infrastructure analysis reveals hidden capacity and utility bottlenecks, helping manufacturers improve uptime, output, quality, and expansion readiness.
- Printing Industry News in 2026: Updates Reshaping Capacity, Costs, and DemandSep 21, 2026Printing industry news 2026: Explore the capacity, cost, packaging, sustainability, and demand shifts reshaping global print operations and investment decisions.